

What Packaging Manufacturers Check Before Approving a New Die
A new die is an important part of folding carton production because it determines where the packaging will be cut, creased, and sometimes perforated. Before a new die is approved for production, packaging manufacturers normally need to check more than whether the overall shape matches the customer's drawing. Small problems in the die can later affect folding, gluing, assembly, and the appearance of the finished carton. The first check is usually the dieline itself. The manufacturer needs to confirm that the cutting lines, crease lines, panel dimensions, flaps, and other structural elements correspond with the approved packaging design. If the dieline contains an incorrect measurement or an unnecessary line, producing a new die before resolving the issue can create problems that are repeated on every sheet.
The overall dimensions of the carton are checked carefully as well. Length, width, and height need to match the agreed specifications, while individual panels must have suitable proportions. The manufacturer also looks at whether the glue flap, locking tabs, dust flaps, and other structural components have enough space to function correctly after cutting and folding. Crease positions receive particular attention because they control how the carton folds. A cutting die can produce a visually accurate flat blank, but poorly positioned or unsuitable creasing can make the finished carton difficult to assemble. Manufacturers therefore need to consider the paperboard grade and thickness when determining whether the planned crease configuration is appropriate.
The direction of the paperboard grain is another practical consideration. Depending on the carton structure, the grain direction can influence folding behavior and the finished carton shape. The die layout therefore needs to be considered together with the sheet layout and material specification rather than being treated as a completely separate part of the project. Manufacturers also check the relationship between cutting and creasing elements. These lines must be positioned accurately so that the carton can move from a flat sheet to its intended three-dimensional shape. If a crease is too close to a cut line or another structural feature, it may affect the strength or folding behavior of the finished package.
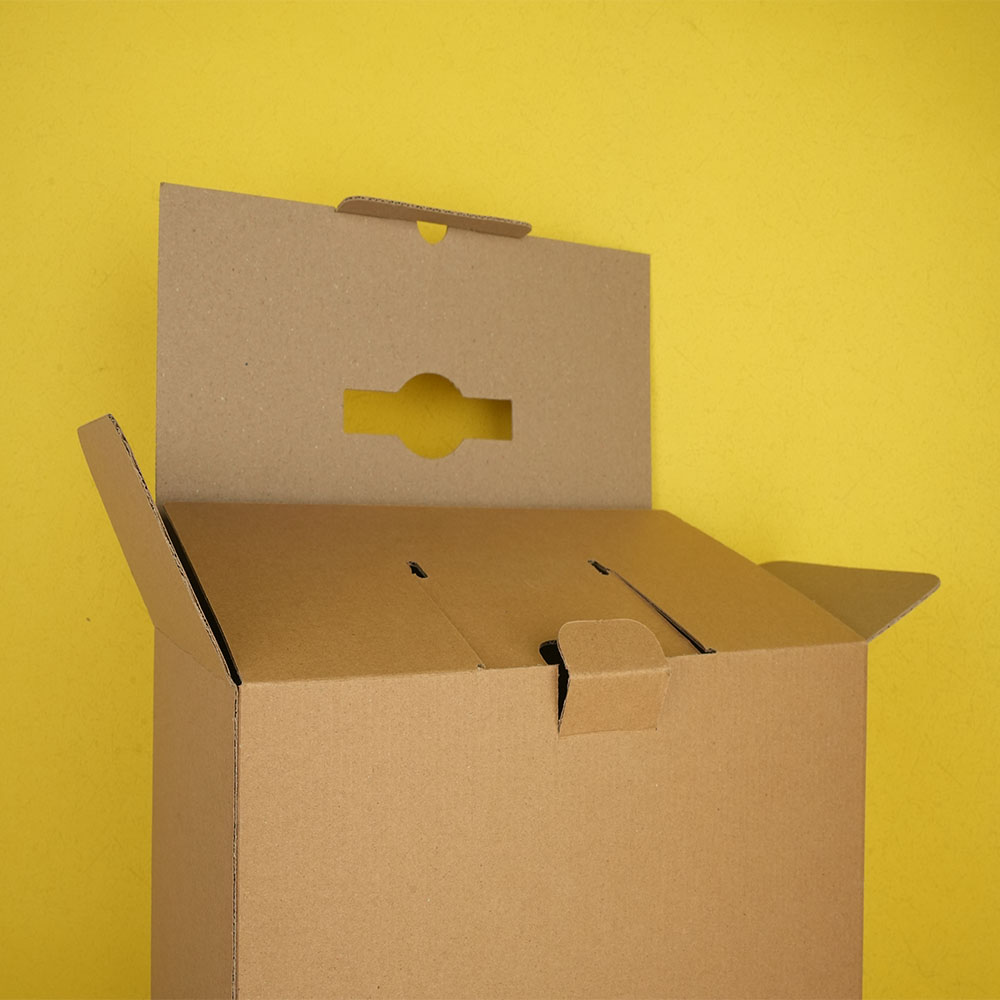
The glue area is another part that deserves attention before the die is approved. A glue flap needs sufficient width and suitable positioning to allow reliable bonding without interfering with other panels. If the flap is too small, bonding can become difficult; if it is too large, it may overlap with another section when the carton is folded. Special structural features require additional checks. Locking tabs, curved edges, windows, perforations, tear strips, hanging holes, and other customized elements can make a die more complicated than a standard carton. Each feature needs to be reviewed to ensure that it can be cut cleanly and will work as intended after folding and assembly.
The arrangement of the carton on the printing sheet is also considered. A manufacturer needs to determine how efficiently the new die can be positioned on the selected sheet size. Poor utilization may increase material waste or limit the number of cartons that can be produced from each sheet. This is particularly relevant for high-volume orders where small differences in material utilization can accumulate quickly. The manufacturer may also review how the die will interact with downstream equipment. The finished blanks need to work with stripping, folding, gluing, and packing processes where applicable. A structure that looks fine on a drawing may still create feeding or folding difficulties if its geometry is not suitable for the production equipment.
Before final approval, the die may be tested through a sample or trial run. This provides an opportunity to examine the actual cut and crease results rather than relying entirely on digital drawings. The sample can be folded by hand or processed through relevant equipment to check whether the carton reaches the intended shape and whether any areas require adjustment. Material compatibility is another important part of the review. A die designed for one paperboard thickness or construction may not produce the same result when used with another material. Cutting pressure, crease configuration, folding behavior, and finished rigidity can all change when the substrate changes, so the approved material specification should be connected to the die design.
A new die is therefore not simply a tool made from a finished drawing. It is part of a larger production system involving paperboard, printing, cutting, creasing, folding, gluing, and packing. By checking the structural dimensions, crease positions, material compatibility, sheet utilization, special features, and production requirements before approval, packaging manufacturers can reduce the risk of costly changes once mass production has started.