

The Practical Challenges of Printing Large Solid Colors on Cartons
Large areas of solid color can give a carton a strong and recognizable appearance, but they can also be surprisingly difficult to print consistently. A small variation that is barely visible on a brochure may become obvious when the same color covers most of a folding carton. For packaging manufacturers, the challenge is not simply putting enough ink on the sheet. It involves controlling the paperboard, ink coverage, printing conditions, drying, and finishing process at the same time. One of the biggest concerns is maintaining an even color across the entire printed area. When a large panel is covered with one solid shade, differences in ink density can create visible light and dark areas. This is especially noticeable with deep colors such as black, navy blue, dark green, and other strong shades. Because there are few graphics or images to distract the eye, even relatively small variations can stand out on the finished carton.
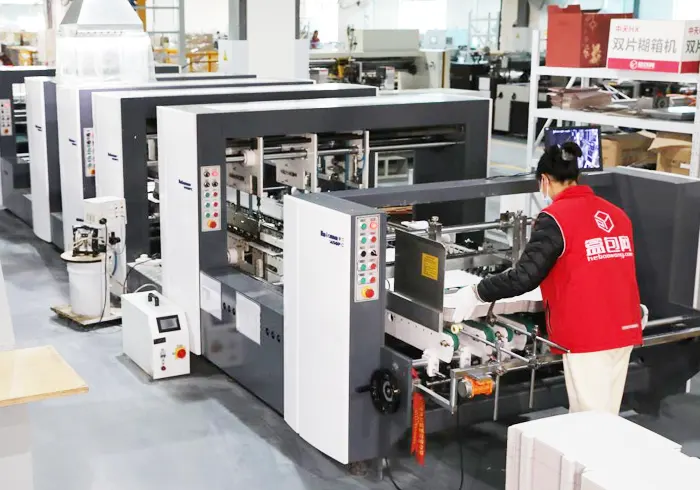
The paperboard selected for the job can also affect the final result. Surface smoothness, coating, brightness, and ink absorption all influence how a color appears after printing. A color that looks correct on one board may appear slightly different on another. This is why changing the paperboard specification during production should not be treated as a simple material substitution, particularly when the carton contains large solid-color panels. Ink coverage needs careful control as well. Large solid areas require stable ink application throughout the printing run. If the ink distribution changes across the sheet or during production, the finished cartons may show differences in color density. Printing equipment, ink settings, plate conditions, and production speed all have a role in maintaining consistency, especially when a large order requires many sheets to be printed.
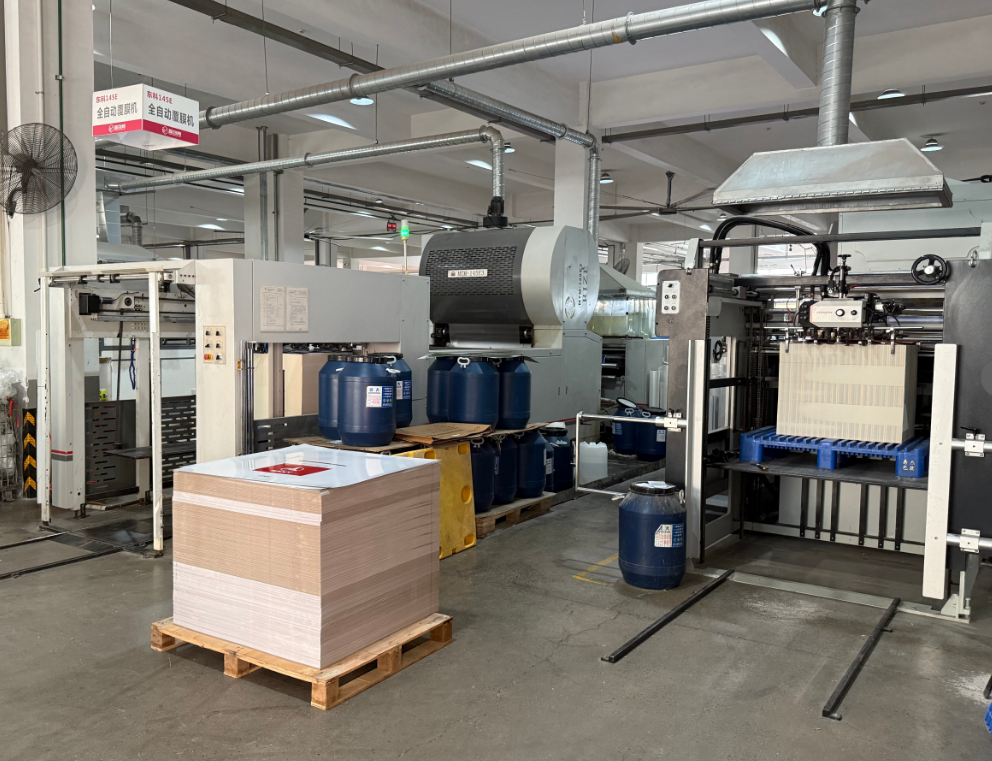
Drying and handling can present another practical challenge. A carton design with extensive ink coverage places more ink on the printed surface than one containing mainly text and small graphics. The printed sheets therefore need to be handled appropriately before moving into later operations. If the surface is not ready for the next process, problems can appear during stacking, coating, cutting, folding, or other converting stages. Large solid colors also make surface defects easier to notice. Small scratches, dust, paperboard marks, uneven coating, or minor handling damage may become highly visible against a uniform background. On a carton filled with photographs and detailed graphics, the same small imperfection might attract much less attention. This makes material cleanliness and careful sheet handling particularly important for solid-color packaging.
Printing registration becomes another consideration when the solid background is combined with text, borders, logos, or other colored elements. Even a small registration difference can be noticeable where two colors meet or where fine details are positioned over a large background. Stable equipment operation and accurate setup are therefore important when the design contains both large color fields and precise graphic elements. The finishing process can further change the appearance of a solid color. Matte coating, gloss coating, varnishing, and other surface treatments can alter how light reflects from the carton. As a result, the same printed color can give a different visual impression after finishing. For this reason, color approval should ideally consider the intended finishing treatment rather than evaluating the printing alone.
Repeat orders can be particularly challenging for brands that expect cartons produced at different times to look almost identical. Production conditions may change between orders, while paperboard batches and other materials can also vary within normal manufacturing tolerances. Keeping clear color references, material specifications, approved samples, and production records gives the manufacturer a better basis for maintaining consistency from one order to the next. The design stage can also influence how easily a solid color can be reproduced. Depending on the required appearance, quantity, printing process, and substrate, a manufacturer may discuss whether a color should be produced using process colors or a specified spot color. The decision should be made according to the actual packaging requirements rather than simply following the method used on another product.
Quality inspection is especially valuable when large solid areas are involved. Instead of waiting until the entire order has been printed, production teams can check sheets during the run for color density, registration, surface defects, and other variations. Early inspection allows adjustments to be made before a small issue develops into a large quantity of potentially unacceptable cartons. For packaging buyers, it is useful to provide clear information about the required color and finishing from the beginning. An approved sample, color reference, paperboard specification, coating requirement, and acceptable tolerance can give the printer a practical standard to follow. If color consistency is critical for a brand, this should be communicated before production rather than after the cartons have been manufactured.
Large solid colors can make packaging look clean, bold, and distinctive, but they leave little room for inconsistency. Successful carton printing depends on several factors working together, from paperboard selection and ink control to registration, drying, finishing, and inspection. When these details are considered before production begins, packaging manufacturers can achieve more stable results and buyers can avoid many of the problems that become difficult and expensive to correct after a large production run.